显示标签为“CBN insert”的博文。显示所有博文

2016年10月20日星期四

Hard turning hardened steel after heat treating used CBN insert Grade
Part 1 The problems of CBN insert hard turning hardened steel
1.Hardened steel problems: High hardness; interrupted turning process; Large deformation;
2.Cutting Tools difficulties: Carbide insert has low hardness; Ceramic insert has large brittleness; Traditional cbn insert will be easily chipping.
Part 2 The solutions of Halnn CBN insert hard turning hardened steel after heat treating
Specific to the current problems on hard turning hardened steel after heat treating, Halnn researched special cbn insert ,and offer the effective solutions as follows:

CBN insert grade
Machining Process
Advantages
Application industry
Insert Picture
BN-H10
Finishing
Suit for finishing with high speed, balance the wear resistance and Collapse resistance
Bearing , gear, gear shaft, constant speed coupling, pearlite ductile cast iron

BN-H21
Finishing
The tips has excellent strength and performance well in interrupted turning conditions
Gear and gear shaft ,mold steel
BN-H11
Finishing
It has more flexible with the cbn insert clamping way, higher machining accuracy, more than one tip
Bearing, Gear, Gear shaft, Constant speed coupling, hardened abrasive

BN-H20
Finishing
it has a good wear resistance and crack resistance when hard turning hardened steel
Brake disc, brake drum, cast iron parts, chilled steel gear
BN-S20
Finishing & Roughing
It has a good chipping resistance and fracture-resistant in a high temperature
Hardened steel rolls, ball screw, wind power bearing ,high speed steel rolls

BN-S200
Finishing & Semi-finishing
It has a better wear resistance when hard turning hardened steel and heat resistance alloy
Slewing bearing, forged chilled rolls ,sintered tungsten carbide

More information ,please check http://www.halnntools.com/pro/
Any questions on hard turning hardened steel or quenched steel ,you can feel free contact with us halnntools@gmail.com ,skype:cbn_inserts_angels .


2016年9月26日星期一

Better performance on hard turning hardened steel with CBN insert 


For high speed machining ,manufacturers have 2 purposes:

1. Lower the cost through improving processing efficiency. Mainly used for finishing process, such as finish turning hardened steel gear ,bearing and mold tools industry.
2. Improve competitiveness through saving processing time and processing costs. Mainly used for roughing process, and choose the most suitable cutting tools materials.

In current times, there are carbide cutting tools, coated carbide insert, ceramic insert. When we choose cutting tools materials, we need to consider so many factors: insert structure, cutting parameters and the cut type, all will affect high speed machining process. So it is an important part of high speed machining technology.

When high speed machining, the work piece rotate with high speed, and it will produce large amount cutting heat. So it will be a key factor that how to take off these heat quickly. So when choose cutting tools materials, we not only need to choose the most suitable cutting tools materials, but also need to choose the suitable angle.

Cutting tools can be ranked depending on different factors.

As hardness: CBN insertCeramic insertsCoated carbide toolsCarbide cutting tools
As roughnessCarbide cutting toolsCoated carbide toolsCeramic cutting toolsCBN insert

As the previous technology, many manufactures will think that cbn insert has bad roughness and it will easily chipping. That is true, previous cbn insert only can be used for finishing and continuous process. But with the development of CBN insert ,Halnn researched new cbn insert materials-solid cbn insert which can be used for finishing and interrupt turning process through continuous research and practices. Solid CBN insert can be used for large allowance roughing and heavy interrupted turning high hardness materials with high speed.

Specific to current cutting tools materials, only cbn insert can performance well on high speed machining and also meet the requirement of “Green manufacturing”.

CBN Insert insert grade which can be used for high speed hard turning hardened steel :

BN-H21 and BN-10 CBN insert belongs to compound cbn insert, it has good hardness with the cutting edge, and also has a good performance with high speed finish turning process.

BN-H11 belongs to soldering cbn insert ,it is more flexible and has better machining accuracy when high speed machining.

BN-S20 and BN-S200 belongs to solid cbn insert, it has a good impact resistance and wear resistance for finishing and semi-finishing.

Solid CBN insert has already researched about 10 years ago, it is non-metal adhesive cbn insert. Especially BN-S20 Solid CBN insert which can be used for heavy interrupted turning hardened steel gear with hardness HRC60,get trust from many manufacturers.

More information on solid cbn insert,http://www.halnntools.com/pro/Solid_CBN_inserts/,Or contact with us halnntools@gmail.com ,skype:cbn_inserts_angels


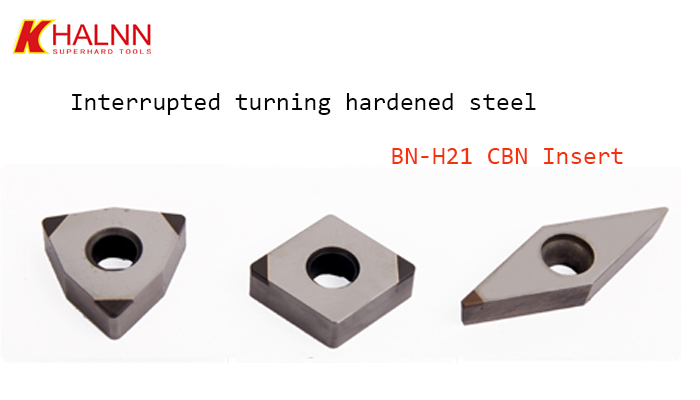
Interrupted turning hardened steel cutting tools--- BN-H21 grade CBN inserts

As we all know, the hardness of hardened steel work piece is high, and difficult to machine, especially for interrupted turning condition, so the requirements on the cutting tools materials improve gradually.

In current times, the materials of machining hardened steel include carbide alloy, ceramic and CBN cutting tools, but because of high hardness of hardened steel, it only suit for CBN inserts .

Hardened steel work piece usually belongs to finish turning after heat-treatment,has small working allowance,and it will be more economical with soldering CBN inserts.But some hardened steel exist interrupted turning condition,such as turning key seating or oil bore on the surface of the work piece.In the process,CBN inserts are easily chipping,so many manufacturers are difficult to guarantee the precision and durability for interrupted turning hardened steel.

But as the manufacturing required product quality increase gradually,it not only require the work piece high precision,but also require product quality improved.Hardened steel,as one of the most common parts in manufacturing is the most important factor which cutting tools enterprise need value.

As a professional CBN inserts manufacturer, Halnn has good development in the following areas: high hardness cast iron/steel, high hardness steel after heat-treatment, cast iron, ect.

Now,as the increase of hardened steel interrupted cutting condition work piece, we researched BN-H21 grade CBN insert which can interrupt turning hardened steel work piece ,and already has good development in gear industry.

http://www.halnntools.com/pro/PCBN_inserts/

Application case as follows: 

1.Workpiece information:

Name: Gear
Hardness:HRC53~61
Other information:φ97.02 ,Depth30mm
Process: finish turning inner bore
Machining condition: semi-interrupted turning
Precision requirement:Ra1.6
Tolerance: +0.02
                    0
2.The cutting parameters of BN-H21 CBN insert interrupt turning gear inner bore

Inserts model:BN-H21 CCGW09T304-2S
Cutting Parameters:
N=500r/min;ap=0.08~0.12mm;Fr=0.08mm/r
Cutting Type:Dry Cutting
Working Efficiency:one cutting edge can machine 180~200piece work piece, and continue working about 3 hours. And guarantee the tolerance and precision requirement, and approval by customers .

More information:http://www.halnntools.com/pro/PCBN_inserts/DNMG.html

2016年9月19日星期一

Rough machining Drum Brake used CBN insert
Drum brake is one of the main parts of the automotive, and belong to consumables, the surface roughness require about Ra1.6.We can choose a suitable insert to get better surface roughness while not affect the manufacture benefit. 

Part 1 Machining drum brake process

In current times, the brake drum brake main materials are gray cast iron. Gray cast iron has good shock absorption and wear resistant, and low noisy, it need simple process.
General process as follows:
Casting-Roughing-Semi-Finishing-Finishing-Drilling-Test.
(1)  Casting: when machining the drum brake, need control the charge mass, also the chemical composition of the molten iron, the pouring temperature, proper ingredients, avoiding casting defects, such as clip sand, porosity, white and so on.
(2)  Roughing: Manufacturers usually use CNC lathe machining the drum brake. Advantages(1.reduce the rejection rate of the work piece, 2.improve the processing efficiency. )
Roughing brake drums need about 0.5mm working allowance for subsequent semi-finishing and finishing guarantee finish requirements.

Part 2 The insert selection of rough machining drum brake

Process the drum brake need three steps,rough machining allowance within 3mm, and the brake drum need a high demand. In the process, it is important to ensure dimension, but improve processing efficiency,
Insert selection required:
1.High-speed cutting
2.Reducing processing time and improving processing efficiency.
First, manufacturers will use carbide insert, but its linear speed is low ,can not satisfy the requirements. So when meet machining gray cast iron with high speed, manufacturer will choose cbn insert which will not only improving the working efficiency, but also save the processing cost.
Especially Halnn BN-S30 and BN-K20 CBN insert, will be more effective for machining drum brake.

Part 3 Select the most suitable cbn insert for different process

(1) Roughing:When the working allowance within 3mm, select BN-S30 CBN insert, which not only has high hardness and high strength, but also has better wear-resistance and impact-resistance. Following show the figure on BN-S30 CBN insert machining brake drum:

Cutting parameters: ap=1-10mm,Fr=0.2-1mm/r,Vc = 200-800m/min. Processing effect: BN-S30 CBN insert lifetime with one cutting edge will be15 times than the coated carbide insert.
(2)Semi-finishing: Working allowance within0.5mm, BN-S30 CBN insert Cutting parameters: ap≤1mm, Fr = 0.05-0.3mm / r, Vc = 300-1500m / min.
(3)Finishing: within margin of 0.3mm, select BN-K20 CBN insert ,which will be more economical, can make sure the braking surface finish and mouth stop finish and dimension tolerances.
Following is the figure of BN-K20 CBN insert machining surface and mouth stopper .

Cutting parameters: ap≤1mm, Fr = 0.05-0.3mm / r, Vc = 300-1500m / min. Processing effect: BN-K20 CBN insert finish turning to ensure roughness Ra1.0, the single cutting edge lifetime is about 2 times than other PCBN insert.
Halnn is the most famous cbn insert brand in China, and always devote to researching new cbn insert to satisfy customers’ requirements.

More information http://www.halnntools.com/pro/,or contact with us halnntools@gmail.com,skype:cbn_inserts_angels