显示标签为“interrupted turning quenched steel”的博文。显示所有博文

2016年9月26日星期一

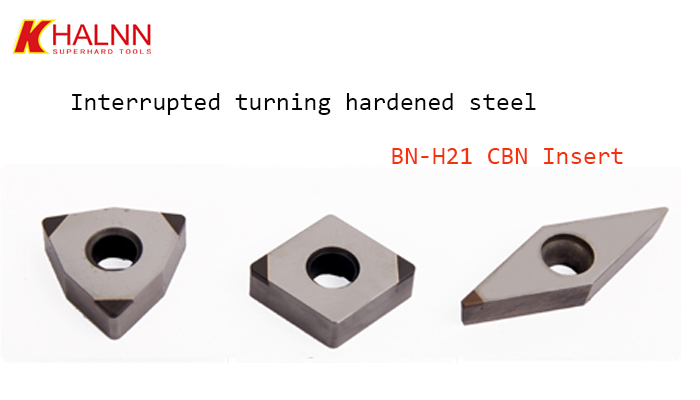
Interrupted turning hardened steel cutting tools--- BN-H21 grade CBN inserts

As we all know, the hardness of hardened steel work piece is high, and difficult to machine, especially for interrupted turning condition, so the requirements on the cutting tools materials improve gradually.

In current times, the materials of machining hardened steel include carbide alloy, ceramic and CBN cutting tools, but because of high hardness of hardened steel, it only suit for CBN inserts .

Hardened steel work piece usually belongs to finish turning after heat-treatment,has small working allowance,and it will be more economical with soldering CBN inserts.But some hardened steel exist interrupted turning condition,such as turning key seating or oil bore on the surface of the work piece.In the process,CBN inserts are easily chipping,so many manufacturers are difficult to guarantee the precision and durability for interrupted turning hardened steel.

But as the manufacturing required product quality increase gradually,it not only require the work piece high precision,but also require product quality improved.Hardened steel,as one of the most common parts in manufacturing is the most important factor which cutting tools enterprise need value.

As a professional CBN inserts manufacturer, Halnn has good development in the following areas: high hardness cast iron/steel, high hardness steel after heat-treatment, cast iron, ect.

Now,as the increase of hardened steel interrupted cutting condition work piece, we researched BN-H21 grade CBN insert which can interrupt turning hardened steel work piece ,and already has good development in gear industry.

http://www.halnntools.com/pro/PCBN_inserts/

Application case as follows: 

1.Workpiece information:

Name: Gear
Hardness:HRC53~61
Other information:φ97.02 ,Depth30mm
Process: finish turning inner bore
Machining condition: semi-interrupted turning
Precision requirement:Ra1.6
Tolerance: +0.02
                    0
2.The cutting parameters of BN-H21 CBN insert interrupt turning gear inner bore

Inserts model:BN-H21 CCGW09T304-2S
Cutting Parameters:
N=500r/min;ap=0.08~0.12mm;Fr=0.08mm/r
Cutting Type:Dry Cutting
Working Efficiency:one cutting edge can machine 180~200piece work piece, and continue working about 3 hours. And guarantee the tolerance and precision requirement, and approval by customers .

More information:http://www.halnntools.com/pro/PCBN_inserts/DNMG.html

2016年8月17日星期三

The research on Interrupt turning quenched steel CBN inserts


Quenched steel, as a kind materials hard to machining, always is a difficult problems in CBN inserts industry ,especially interrupt turning quenched steel.When CBN inserts interrupt turning quenched steel ,it will finish the process with 100 times attack per minute,and it also is a big challenge for the impact resistance of CBN inserts.

Cutting parameters of CBN inserts interrupt turning quenched steel

Workpiece cutting can be divided 3 parts depend on the rate of continuous cutting time:continuous turning,high frequency and low frequency turning ;Section cutting. It continue to obey impact  resistance and vibration in the machining process,and it also appear out parts, moving parts, broken knives ect phenomenon.It has low efficiency and low quality.For example,it has become a trend using turning quenched gears instead of grinding.Even though hard turning quenched steel has been used by many customers ,but it also meet many different problems on machining automobile quenched steel.For example,some automotive Gears has oil bore,which will appear interrupt turning problems,many CBN inserts will chipping when high speed turning gears with inner bore ,and the tolerance can not guarantee,ect.

Research on Interrupt turning quenched steel CBN inserts

1.The hardness of quenched steel can Estimate with HRC=100-37353/(HV+200),we can get very precise result and it is very convenient.

2. CBN inserts selection used for interrupt turning quenched steel
When interrupt turning quenched steel ,We can choose coating carbide alloy inserts and cbn inserts depend on the workpiece hardness and working parameters(Ceramic cutting tools has low impact resistance ,only can continuous finish turning )

(1)Coated carbide alloy cutting tools,suited for machining workpiece which hardness is below HRC45,and it need low speed turning ,if just machining quenched steel occasionallyit can choose carbide alloy inserts,such as YT726.

(2)CBN inserts,suited for hard turning workpiece which hardness is above HRC45,CBN inserts can be divided into 2 kinds,compound cbn inserts,and the cutting depth usually can be below 0.3mm,and it always chipping when interrupt turning .Even though some imported cbn inserts said that they has new grades to interrupt turning ,but many are specific to common interrupt turning,and it need finish turning .In current times ,the customers find it difficult to find a suitable cbn inserts to solve their problems.
Specific to heavy interrupt turning hardened steel problems,Halnn superhard researched BN-S10,BN-S20 CBN inserts to help customers solve their problems. It is a huge step in cutting tools industry.

Figure 1 BN-S20 CBN inserts heavy interrupt turning quenched steel
Large scale gears are heavily deformed after after carburizing, gears outer ring deformation can arrive 2mm,the hardness after quenching can be HRC60~65,cutting speed :50~70m/min,cutting depth:1.5~2 mm Feed rate:0.15~0.2 mm/r, one step can machine all allowance ,the previous ceramic cutting tools just can cut the deformation ,and chipping heavily,the processing cost is very high.

Test result: BN-S20 CBN inserts has better impact resistance than imported CBN inserts, the lifetime can be 6 times than previous cutting tools when cutting depth can add 3 times,the cutting efficiency improved 3 times.The workpiece roughness can arrive the customers requirements. And the best advantage is the failure mode is not chipping ,but normal wear. And the appearance of BN-S20 CBN inserts shocked the cutting tools industry,and make it possible to heavy interrupt hard turning quenched steel .

Figure 2 BN-S20 CBN inserts turning automotive gears end surface inner bore,machining end surface belongs to interrupt turning ,and there is inner hole,it belongs to common interrupt turning, it is used Halnn BN-S20 Welded CBN inserts,finishing .

The relationship of CBN inserts angle with lifetime

When Interrupt turning HRC65 quenched steel parts,the angle of CBN inserts are 0.2*20 Negative chamfer,the inserts holder has Chucking rake angle (-6 degrees) and the rear angle (6 degrees).
IN interrupt turning process ,the main factors on the inserts lifetime are Mechanical impact;When the Negative chamfering is large,the cutting parameters and machine impact effect will be the main factors which affacted the cutting tools lifetime.

More information,http://www.halnntools.com/pro ,Or contact with us halnntools@gmail.com,whatsapp:+8615036165377,skype:cbn_inserts_angels